Discover how advanced control systems improve product consistency, reduce waste, and optimize your extrusion process. Explore our solutions or connect with our team to learn how ICT can modernize your production line.
Get Started TodayA barrel zone is only as good as the device that switches heater power. The temperature controller or PLC decides how much heat a zone needs, but a contactor, solid state relay or SCR power controller turns that decision into current through the heater bands. The choice affects how tightly zones hold setpoint, how often panels need service, and what happens when a component fails. This post covers the main switching options, how to apply them, and the monitoring and safety layers that should surround them.
Contactors were the standard for barrel heating for decades and remain common on older lines. They are inexpensive, tolerant of electrical abuse, and provide a true air gap when open. Their weakness is mechanical life. Every cycle wears the contacts, so contactors are typically run with long time-proportioning cycle times, often tens of seconds, to keep the number of operations reasonable.
Those long cycle times are the core problem. A zone that receives full power for several seconds and then nothing for several more will show temperature ripple, especially where thermal mass is low or the heater sits close to the thermocouple. The controller can only correct as fast as the output allows, which limits how well the zone can be tuned.
Many older extruders used mercury displacement relays, where a magnetic plunger displaced liquid mercury to close the circuit. With no exposed contacts to pit or weld, they handled faster cycling better than early contactors. However, mercury is hazardous and restricted in many places, a cracked relay creates an exposure and cleanup problem, and replacements are increasingly hard to source. During a controls upgrade they are usually replaced with heat-sinked SSRs, and the removed relays should go to a qualified hazardous waste handler.
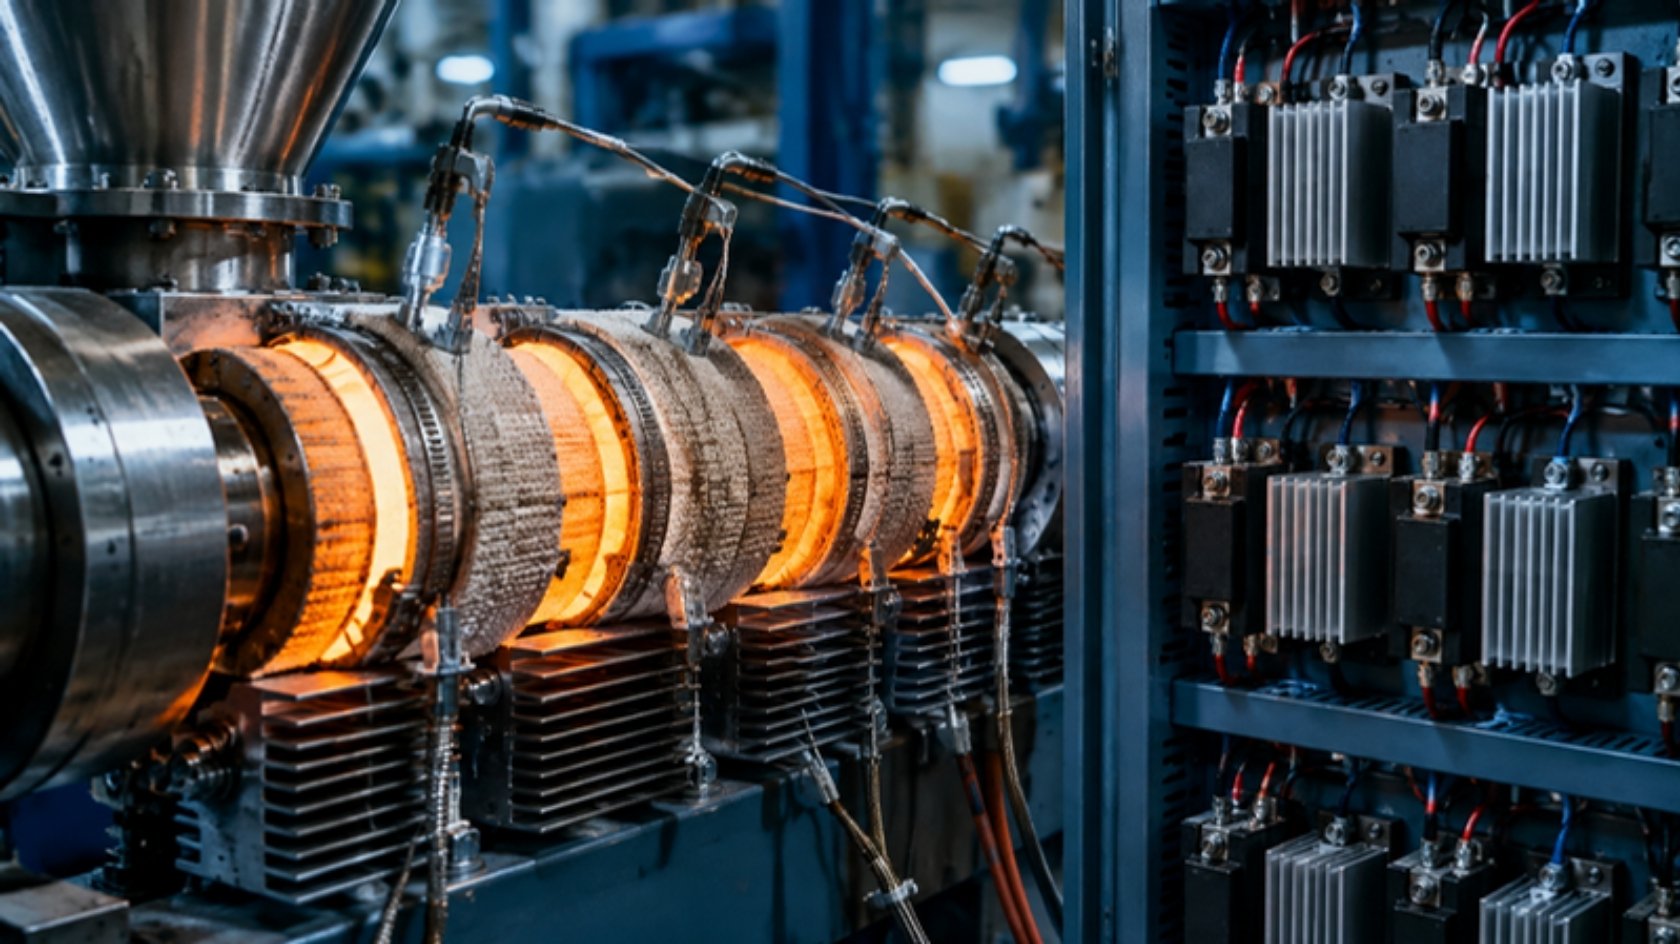
A solid state relay switches AC power with semiconductors, so it has no mechanical wear. Most barrel heating SSRs are zero-cross types, which turn on near the zero point of the voltage waveform and turn off at the next current zero, keeping electrical noise low with resistive heaters. Cycle times of a second or two are common, and many controllers can go shorter.
Faster cycling smooths the power delivered to the heater, makes the zone easier to tune, and reduces thermal cycling of the heater element itself. For most barrel zones, a properly sized and cooled SSR is the default choice on new and retrofitted systems. For more on tuning once the output is fast enough, see our post on PID tuning for extruder barrel zones.
An SCR power controller packages back-to-back thyristors with heat sinking, firing circuitry and often fusing and current monitoring, and it accepts an analog or digital power command. Burst firing passes whole AC cycles in a pattern that averages to the commanded power, effectively very fast time-proportioning. Phase angle firing turns the thyristors on partway through each half cycle for continuously variable voltage.
Phase angle control suits loads with low cold resistance, transformer-coupled loads, or heaters that need soft starting, but it generates harmonics that ordinary resistive bands rarely justify. SCR controllers earn their place on large or high-current zones and where integrated diagnostics in one device are valuable.
When an SSR conducts, its semiconductor has a forward voltage drop of roughly a volt or more, and that drop times load current is dissipated as heat. A relay carrying tens of amps produces tens of watts continuously. The nameplate current applies under specific test conditions, and manufacturer derating curves show usable current falling as ambient or heat sink temperature rises. Size SSRs with generous headroom, verify heat sink thermal resistance against the curve for the real panel temperature, use thermal compound or pads, mount sinks with fins vertical, and keep panel filters and fans maintained. Semiconductor-rated fuses are the usual short-circuit protection, since ordinary breakers react too slowly.
Overheating, voltage transients and overcurrent most often leave an SSR output shorted, so the heater stays on regardless of the controller command. The zone runs away in temperature, which can degrade material, damage the screw or barrel, or create a fire risk. SSRs also have a small off-state leakage current, so a heater circuit is never de-energized just because the SSR is off.
Because the primary switching device can fail on, overtemperature protection must not depend on it. The standard approach is an independent high-limit device with its own sensor that drops out a contactor upstream of the SSRs or SCRs. That contactor stays closed during production, so it sees few operations and remains reliable. The high limit should require manual reset and should not live only in the same controller or PLC logic that drives the heater outputs. Our post on safety interlocks in extrusion covers how these layers fit into broader machine safeguarding.
Barrel zones often have several bands in parallel. When one burns out, the rest can frequently still hold setpoint at a higher duty cycle. The display looks normal, but the zone has lost reserve capacity and heats unevenly, and the next failure may cause a real deviation. Rising output percentage is a clue, but an indirect one.
A current transformer on each zone gives a direct measurement. With the output on, the controller compares measured current to the expected value and alarms on a drop, revealing a failed band, open connection or blown fuse. With the output off, any measured current indicates a shorted SSR, giving warning before the high limit trips. Many temperature and SCR controllers accept CT inputs directly, and PLC systems can read them through analog or heater current modules.
Set the alarm threshold between normal zone current and the current with one band missing, so a single failure is caught without nuisance alarms from supply variation. The measurement must be synchronized with the output state or averaged over on time, and recording expected current per zone at commissioning speeds later troubleshooting.
Smaller zones are often single-phase, while larger zones and dies may use three-phase heaters in delta or wye. Three-phase zones are switched on all three legs or, commonly, on two legs with the third connected directly. Two-leg switching saves a device, but the heater is never isolated by the switching devices alone, another reason the upstream contactor and lockout procedures matter. Heater break monitoring should cover more than one leg.
Many single-phase zones should be distributed across the three supply phases so phase currents are as close as practical. Imbalance raises line or neutral currents, can cause voltage imbalance for other equipment, and wastes supply capacity. Some controllers can also stagger the start of time-proportioning cycles so zones do not all switch on at once, reducing peak demand.
Air-cooled barrels use blowers, which are motor loads usually switched with contactors or motor starters on longer cycle times than heating. Water-cooled zones use solenoid valves, where cycle time and minimum pulse length need care to limit valve wear and abrupt cooling. Small solenoid coils can be held in by SSR leakage, so relay outputs or SSRs rated for low-current loads fit better.
A practical review starts with an inventory of each zone's switching device, cycle time, heat sinking and protection. Warning signs include discolored SSRs or wiring, missing thermal compound, contactors on short cycle times, mercury relays, and high limits that share a controller with the process loop. Zones without current monitoring are candidates for CT retrofits, especially with multiple bands per zone.
Upgrades are most efficient when power switching, monitoring and safety circuits are designed and documented together. ICT builds extruder control systems with properly sized SSR or SCR heater control, per-zone current monitoring, independent high-limit protection and coordinated cooling outputs, integrated with the PLC and HMI.
In most cases, yes. SSRs allow much shorter cycle times, which improves temperature stability, and they do not wear mechanically. Keep a contactor upstream for high-limit and isolation duty, and size SSR heat sinking carefully.
SSR outputs are commonly set to a second or two, and zero-cross devices can go shorter. The goal is a cycle time short relative to the zone's thermal response, so check the controller documentation and retune after any change.
SSRs most often fail shorted, leaving full power on the heater regardless of controller output. An independent high limit that opens a separate contactor protects against this, and CT monitoring can detect current while the output is off.
SCR controllers suit large or high-current zones, loads needing phase angle firing or soft start, and applications where integrated fusing and diagnostics add value. For standard resistive band heaters, a well-applied SSR usually provides comparable control.